How to Choose a 3D Five-Axis Laser Cutting Machine: Working Range, Accuracy, Table and Laser Power
-
September 9, 2026

-
26 min read

Choosing a 3D five-axis laser cutting machine is fundamentally different from choosing a conventional flatbed laser cutter.
For flat sheet, buyers often begin with relatively straightforward questions:
For a three-dimensional formed component, those questions are only the beginning.
The cutting head may need to:
This means the correct machine depends on the complete relationship between:
Part geometry + machine travel + cutting-head motion + fixture + worktable + laser process + production strategy
A machine with more travel or more laser power is not automatically the better choice.
A successful selection process starts with the actual component.
Before comparing five-axis models, prepare a clear description of what the machine must process.
At minimum, define:
This is especially important for components such as:
ZG Laser’s current five-axis range is organized around different production scenarios rather than one universal machine: automotive hot-formed production, general industrial 3D cutting, small-to-medium batch work, compact production and non-metal applications.
Instead of asking:
“Do I need a 3000W or 6000W five-axis machine?”
start with:
“What complete three-dimensional cutting task must the machine perform?”
Laser power should be selected later.
For several product families, create a simple requirement matrix.
| Requirement | Information to Record |
|---|---|
| Part type | B-pillar, panel, tube, mold, structural part |
| Material | Carbon steel, stainless steel, aluminum, etc. |
| Thickness | Minimum / typical / maximum |
| Part size | X × Y × Z overall envelope |
| Fixture size | Approximate footprint and height |
| Cutting features | Trim, holes, slots, bevels |
| Required tolerance | Critical vs general features |
| Annual volume | Parts/year |
| Production rate | Parts/shift or target cycle time |
| Loading | Manual / robot |
| Variants | Number of different parts |
The machine should be optimized around the parts that represent most of your production—not around one rare oversized component.
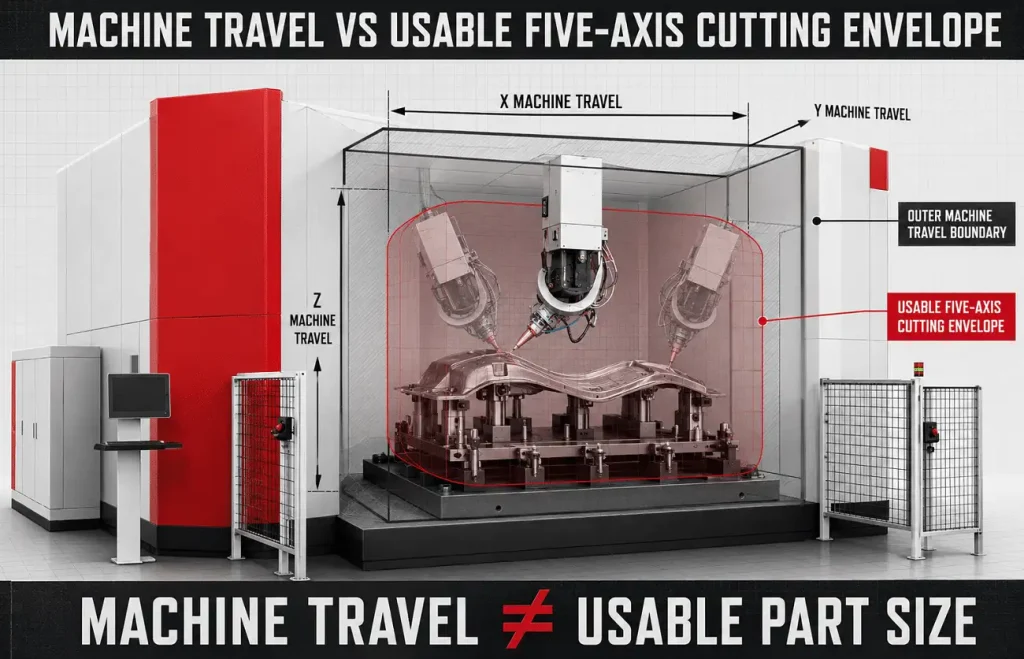
This is one of the most important points in five-axis machine selection.
A specification may state:
That does not automatically mean a 4500 × 2500 × 700 mm workpiece can be processed in every orientation.
The actual usable part size also depends on:
Your current S-Auto page draft already makes this distinction explicitly: the part, fixture and cutting-head clearance must be considered together when confirming the usable cutting envelope.
A better engineering concept is:
Usable Cutting Envelope = Machine Travel − Fixture Constraints − Cutting-Head Clearance − Motion Safety Margin
This is conceptual rather than a literal subtraction formula, but it reflects how the project should be evaluated.
Do not send only the part dimensions to the machine supplier.
Consider the part-and-fixture assembly.
For example, a component may measure:
2800 × 900 × 400 mm
but after fixture design the complete installation may occupy:
3300 × 1300 × 650 mm
because the fixture includes:
Then add cutting-head movement around the fixture.
The final required machine envelope may be much larger than the raw part dimensions suggest.
X/Y/Z travel determines the linear working envelope.
Usually influences the maximum usable component length.
Important for:
Determines width access.
This becomes important when:
Z travel is easy to underestimate.
It must accommodate:
A 500 mm-high part on a 250 mm fixture does not automatically fit into a machine with 700 mm Z travel.
The complete kinematic model must be checked.
A five-axis machine usually adds two rotary movements to X/Y/Z.
ZG Laser’s current fiber five-axis platforms list A-axis travel up to ±135° and continuous multi-turn C-axis capability on several configurations.
The specific axis naming can vary between machine manufacturers.
What matters is whether the cutting head can reach every required surface.
Do not validate only easy trim contours.
Identify features such as:
Then simulate the required cutting-head orientation.
A very large rotary range creates no value if your parts do not require it.
What matters is:
Can the machine reach all required cutting features without approaching axis limits or causing collisions?
A five-axis machine can have enough nominal travel but still fail to access one important feature.
Possible causes include:
This is why a 3D machine selection project should include:
Part model + fixture model + cutting-head model + machine model
before final configuration.
Offline programming and collision simulation
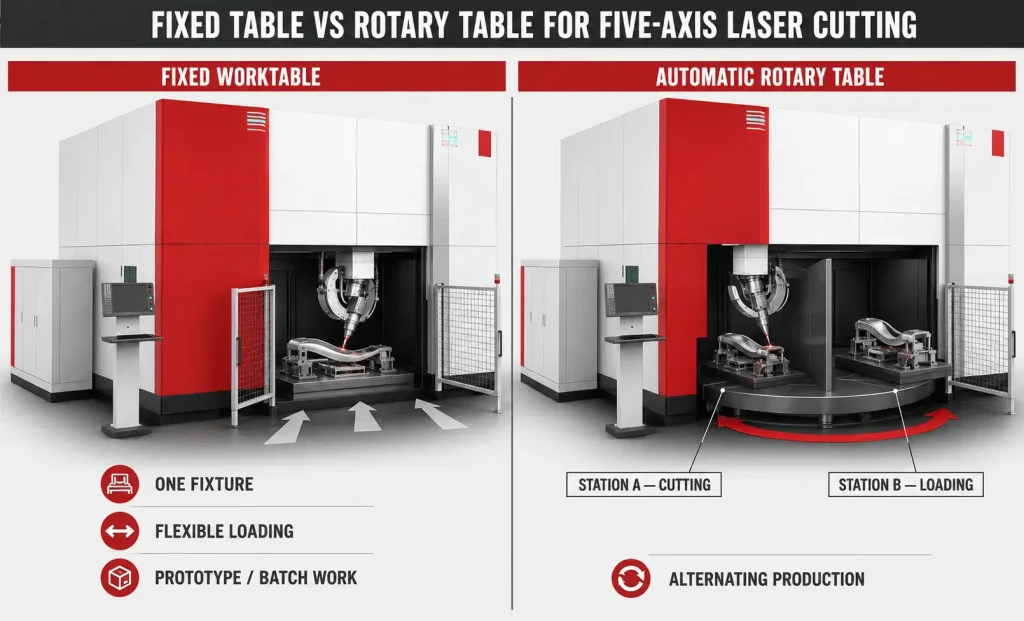
Two five-axis machines may both physically fit the part but be intended for very different production strategies.
For example:
Machine A
Machine B
If the project produces:
20 prototype parts per month,
Machine B may provide little economic benefit.
If it produces:
hundreds of hot-formed components per shift,
the rotary-table architecture can become much more valuable.
Therefore:
Working range determines whether the machine can process the part. Production architecture determines whether it should process the part.
Accuracy is another specification buyers frequently misinterpret.
A brochure may provide:
These are useful machine specifications.
But they are not automatically finished-part tolerances.
ZG Laser’s current five-axis specifications, for example, list X/Y/Z machining accuracy of ±0.05 mm and repeat positioning accuracy of ±0.03 mm for several fiber models.
Those values describe machine-axis performance.
The finished component also depends on:
Your existing five-axis accuracy article explains this distinction in detail.
Ask:
“Can the complete process repeatedly meet the critical tolerances on my actual component?”
Not every feature requires the same tolerance.
Separate the drawing into:
Examples:
Examples:
This matters because achieving very tight tolerance everywhere may require:
The project should optimize accuracy where it creates functional value.
A supplier may produce one excellent sample.
That proves feasibility.
It does not necessarily prove production stability.
For repetitive production, evaluate several consecutive parts.
Record:
A machine suitable for one prototype is not automatically suitable for mass production.
The worktable is one of the most important configuration decisions.
Common options include:
ZG Laser’s current portfolio uses different worktable concepts across its five-axis platforms: the S-Auto family uses an automatic rotary table, DF configurations can use fixed or slide worktables, and SF is positioned around a fixed worktable.
A fixed table is a strong starting point when:
Advantages can include:
A fixed table does not mean the machine is low productivity.
For parts with long laser-on times, loading may represent only a small share of the total cycle anyway.
A sliding table can improve loading access or support alternative production layouts.
Possible benefits include:
The actual benefit depends on the specific table mechanism and machine layout.
Ask:
Do not assume “slide table” means the same thing on every machine.
A rotary table becomes particularly attractive in repetitive production.
The concept is simple:
Station A: Cutting
while simultaneously:
Station B: Unload finished part + load next part
Then the table indexes.
This reduces the amount of time the cutting machine waits for the operator.
ZG Laser’s S-Auto platform uses an automatic rotary-table architecture and is positioned around automotive hot-formed parts and high-cycle production.
Your current S-Auto configuration draft lists 4,000 mm and 5,000 mm table diameters for its two machine sizes, with single-side load capacities of 350 kg and 500 kg respectively.
This distinction matters when reviewing brochures.
A rotary table may index very quickly.
That does not mean the complete part cycle is equally short.
The actual production cycle includes:
Loading + Positioning + Clamping + Table Indexing + Piercing + Cutting + Head Repositioning + Unclamping + Unloading
Your current S-Auto technical draft already includes a note that table positioning time should not be interpreted as total cutting or production cycle time.
Always request:
complete part cycle time
rather than one motion-system speed.
Large automotive fixtures can become heavy.
The table must support:
For multi-station tables, verify whether the specification refers to:
Do not compare only table diameter.
A larger fixture may physically fit but exceed permissible load or reduce machine dynamics.
ZG Laser’s current fiber five-axis portfolio offers 3000W, 4000W and 6000W configurations across several product families.
But power selection should come after you have established:
Why?
Because laser power primarily affects the cutting process.
It does not solve:
Material thickness matters, but it is only one variable.
Power selection should consider:
Two parts made from the same thickness can require different configurations.
Part A
Part B
The same nominal thickness does not make them the same laser application.
Do not publish a universal thickness table for these three powers unless it has been validated for the exact machine, material and process.
A better buyer-guide framework is:
May be evaluated where:
May offer a useful middle configuration when:
May deserve evaluation when:
These are evaluation directions, not fixed material capability limits.
The final choice should be validated through sample testing.
Suppose laser power reduces actual cutting time from:
60 seconds to 45 seconds.
But the complete cycle also requires:
The improvement in total productivity is much smaller than the raw cutting-speed improvement suggests.
This becomes especially important in 3D processing because:
Compare total cycle time, not maximum laser speed.
Typical fiber-laser cutting gases include:
ZG Laser’s DF and SF five-axis specifications currently list air, nitrogen and oxygen as applicable assist gases.
Gas selection affects:
A 6000W machine operated with expensive nitrogen is not automatically more economical than a lower-power configuration using a different validated process.
Evaluate cost per acceptable finished part.
Laser Cutting Assist Gas: Oxygen vs Nitrogen vs Compressed Air
Five-axis brochures may list:
These indicate machine dynamic capability.
They do not directly equal production speed.
ZG Laser currently lists maximum linear-axis speeds of up to 100 m/min for some five-axis configurations and 80 m/min for others, with A/C-axis speeds up to 540°/s on several fiber platforms.
But real cutting involves:
Therefore:
maximum axis speed is a machine capability specification—not a guaranteed part-production rate.
A long straight rapid movement benefits from high linear speed.
A small complex automotive component may instead require:
In this case:
may influence cycle time more than top linear speed.
Ask the supplier to run your complete part program when cycle time is important.
For 3D five-axis cutting, offline programming is not an optional convenience for complex production.
It is a core engineering capability.
The programming system should support functions such as:
ZG Laser’s current five-axis product page lists offline programming, five-axis control and process-parameter settings among the system capabilities for complex 3D geometries.
Confirm:
Offline Programming and Collision Simulation for 3D Five-Axis Laser Cutting
Five-axis systems process parts at different orientations.
This can change the direction of:
Evaluate:
ZG Laser currently offers safety enclosure and dust-extraction options according to system configuration.
The correct configuration depends on:
Automation should solve a production bottleneck.
A five-axis machine can also be combined with a separate handling robot.
This allows:
five-axis machine = cutting
and:
robot = loading/unloading
The production cell should be designed around the full cycle rather than machine capability alone.
Before ordering a dedicated machine, very large or highly variable parts should also be evaluated against robotic cutting.
A dedicated five-axis machine generally provides:
A robotic system may provide:
Neither is universally superior.
For the current ZG Laser portfolio, a practical selection logic is:
| Production Scenario | Starting Platform |
|---|---|
| Automotive hot-formed parts / high-cycle production | S-Auto Series |
| General industrial 3D parts / larger flexible processing | DF Series |
| Prototype / small-to-medium batches | SF Series |
| Smaller parts / limited workshop space | Compact Five-Axis |
| Non-metal 3D processing | CO₂ Five-Axis |
| Extremely large or highly variable 3D components | Also evaluate robotic laser cutting |
ZG Laser’s current collection page positions the series in broadly these application groups.
The S-Auto architecture is intended for repetitive automotive 3D trimming.
Typical applications include:
The current product family uses:
ZG Laser currently lists approximately 3500–4500 mm X travel, 2100–2500 mm Y travel and 700 mm Z travel across the S-Auto range.
The main purchasing question is not:
“Is S-Auto the highest-spec machine?”
It is:
“Does my production volume justify a dedicated rotary-table automotive architecture?”
DF is positioned toward broader industrial 3D processing.
Applications listed by ZG Laser include:
Current configurations use fixed or sliding worktable layouts and approximately 4000–4500 mm X travel, depending on model.
DF may be a better starting direction when:
SF is positioned toward:
The current machine architecture uses a fixed table and 3 / 4 / 6 kW fiber-laser configurations.
It may be appropriate when the buyer needs true five-axis capability but does not need the more production-oriented architecture of an automotive rotary-table system.
This can be particularly relevant for companies entering 3D laser cutting for the first time.
Large working range is not free.
It can increase:
ZG Laser’s current compact platform lists approximately:
1500 × 1500 × 700 mm X/Y/Z travel
with 3000–6000W fiber-laser options.
If your workpieces are consistently small, a compact system may provide a more rational production footprint.
Do not buy 4.5 meters of X travel simply because it looks more capable.
Do not assume every five-axis laser machine is designed for metal.
ZG Laser also lists a CO₂ five-axis platform for materials such as:
The current CO₂ configuration is fundamentally different from the 3–6 kW fiber-metal systems and is listed at 200W in the current product table.
Select laser technology according to material first.
Do not compare only the number of axes.
A machine that fits the part may not fit the workshop.
Include space for:
ZG Laser’s DF and SF specifications show that complete machine footprints can reach several meters beyond the nominal cutting travel.
Always request a complete installation-layout drawing before order.
Depending on machine configuration, prepare for:
Do not wait until the machine arrives to discover that:
Utilities belong in the purchasing decision.
For a serious five-axis project, catalog comparison should lead to sample validation.
Provide the supplier with:
ZG Laser’s current project-evaluation process likewise recommends drawing review, configuration review and sample cutting for critical projects.
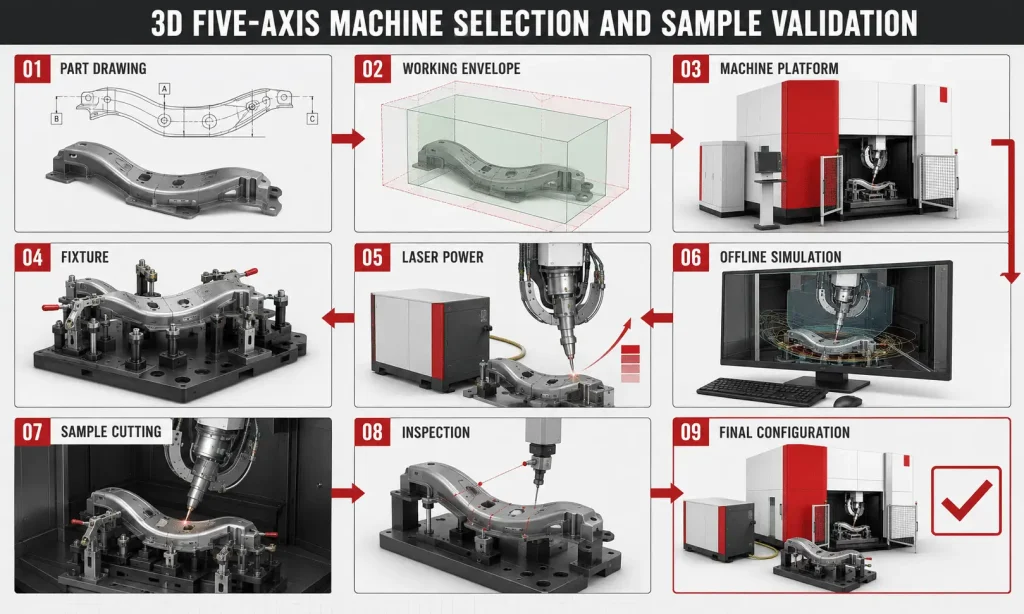
If the component contains:
the difficult feature should drive feasibility testing.
A supplier demonstration showing only an easy external cut does not prove the machine can process the complete part.
Include:
in the test program.
Do not wait until after sample cutting to decide whether the result passes.
Agree in advance on:
This prevents situations where:
the supplier measures from one datum,
while:
the customer later measures from another.
Factory Acceptance Testing should include machine checks.
But for a custom 3D production project, part-level validation is often more meaningful.
Possible FAT items include:
Do not allow an application-specific machine to be accepted only because the axes move correctly.
Five-axis system cost can include:
Operating cost can include:
The relevant metric is:
Cost per acceptable finished part
not:
Machine price per kilowatt
Consider two machines.
Lower purchase price, but:
Higher purchase price, but:
For high-volume production, Machine B may have the lower cost per part.
For small batches, Machine A may be the better investment.
This is why machine architecture should follow annual production volume.
Before finalizing an order, ask:
A good supplier should explain:
why the recommended configuration fits your part and production strategy.
Before placing the order, confirm:
Choosing a 3D five-axis laser cutting machine should not begin with laser power.
It should begin with the part.
The correct selection sequence is:
Part geometry
→ usable cutting envelope
→ cutting-head accessibility
→ required accuracy
→ fixture strategy
→ worktable architecture
→ production volume
→ laser power
→ software and automation
→ sample validation
A large machine with a high-power laser can still be the wrong solution if:
Likewise, a smaller or lower-power configuration can be the better investment when it matches the real production task.
The most important buying principle is:
Choose the complete production system—not the most impressive individual specification.
For a critical five-axis project, the final machine should therefore be selected only after the supplier has evaluated:
and, where practical, verified the configuration through representative sample cutting.
Send ZG Laser:
Our application team can evaluate:
before recommending a final machine configuration.
Send Your 3D Drawing for Evaluation
Explore 3D Five-Axis Laser Cutting Machines
Start with the actual part geometry, material, thickness, required tolerances, production volume and target cycle time. Then evaluate machine travel, cutting-head accessibility, worktable, fixture, laser power and software as one complete system.
No. Fixture dimensions, cutting-head tilt, clamps, machine structure and required safety clearance reduce the usable processing envelope.
Choose enough X/Y/Z travel to cover the complete part, fixture and cutting-head movement. Avoid significantly oversizing the machine unless future production requirements justify it.
They determine whether the cutting head can reach angled and curved surfaces. Actual accessibility should be checked using the part, fixture and machine model.
No. Machine-axis accuracy is only one contributor. Final part accuracy also depends on calibration, fixture repeatability, workpiece variation, programming, cutting conditions and measurement. ZG Laser’s current five-axis specifications use ±0.05 mm as an X/Y/Z machine-axis accuracy value on several configurations.
A fixed table is often suitable for flexible or smaller-batch production. A rotary table becomes attractive when high-volume production allows loading and unloading at one station while cutting occurs at another.
Not necessarily. Productivity depends on the complete cycle, including loading, clamping, cutting and unloading. Fast table indexing alone does not determine output.
Select power according to material, thickness, cutting features, edge requirements and target cycle time. ZG Laser currently offers these three power levels on several fiber five-axis platforms, but the correct choice should be validated on representative parts.
No. Higher power does not increase working range, improve fixture design or solve head-access problems. It also may not significantly reduce total cycle time when loading, piercing or multi-axis movement dominates production.
A production-oriented system with suitable working envelope, accurate fixtures and efficient loading should be evaluated. ZG Laser currently positions its S-Auto platform specifically for hot-formed automotive structural components and rotary-table production.
A compact configuration can make sense when workpieces are smaller, workshop space is limited and the larger working range of a full-size machine would provide little production benefit.
For complex 3D parts, offline programming and collision simulation are highly valuable because head orientation, fixtures and machine motion should be verified before production.
For critical applications, yes. Representative sample cutting allows you to verify accessibility, edge quality, dimensional results, fixture strategy and cycle time before the final machine configuration is confirmed.
Provide the 3D model, 2D drawing, material, thickness, maximum dimensions, required cutting features, tolerances, annual volume, target cycle time and automation requirements.
For more practical guidance on laser equipment maintenance, troubleshooting, performance optimization, and failure prevention, explore the related technical resources below. These articles provide additional engineering insights to help you improve machine reliability, efficiency, and long-term performance.

English

French

German

Hindi

Italian

Japanese

Korean

Portuguese

Russian

Spanish
Tell us about your manufacturing challenges.
Our engineers will design a laser solution tailored to your exact requirements.