How to Validate a 3D Five-Axis Laser Cutting Machine Before Purchase: Sample Testing, FAT and Acceptance Criteria
-
September 18, 2026

-
24 min read

A 3D five-axis laser cutting machine can look impressive in a brochure.
The specification may show:
But none of these specifications alone proves that the machine can repeatedly process your actual part to the required quality and cycle time.
For complex applications such as:
the most useful validation method is to move from specifications to an actual application test.
A structured validation project should answer several questions:
ZG Laser’s current five-axis project-evaluation process already recommends drawing review, process and fixture evaluation, machine configuration review and sample testing for critical projects.
The next step is to make that validation process measurable.
The key principle is:
One successful sample proves feasibility. Repeated samples begin to demonstrate repeatability. Production capability requires a separately defined validation plan.
A conventional sheet-metal cutting project can often be evaluated using well-established material and thickness data.
Three-dimensional cutting has more variables.
The result depends on:
A machine may have sufficient nominal travel but fail to reach one recessed hole.
It may cut a perfect contour on a rigid demonstration sample but struggle with a variable hot-formed production part.
It may produce acceptable dimensions while loaded in the fixture but fail after unclamping because the component relaxes.
This is why the actual application should be tested before a critical purchase is approved.
How to choose a 3D five-axis laser cutting machine
These three stages should not be mixed together.
Usually occurs during application evaluation.
Its main purpose is to determine:
Can the proposed process manufacture the part?
It may happen before the final order.
FAT takes place at the supplier’s factory before shipment.
Its purpose is to verify that the ordered equipment and agreed application requirements have been met before the machine leaves the supplier.
SAT takes place after installation at the customer’s factory.
Its purpose is to verify that:
are correct at the final site.
| Stage | Main Question |
|---|---|
| Sample Test | Can the proposed process make the part? |
| Repeated Sample Test | Can the process produce similar results repeatedly? |
| FAT | Does the completed machine meet the agreed pre-shipment requirements? |
| SAT | Does the installed machine operate correctly at the customer’s factory? |
The exact scope should always be defined in the purchase agreement.
There is no single universal FAT checklist that applies to every custom five-axis laser project.
The quality of the test depends heavily on the information supplied.
At minimum, provide:
For formed components, actual production samples are extremely valuable.
The nominal CAD model cannot fully show:
ZG Laser’s current project-evaluation page similarly asks buyers to provide drawings, material, thickness, maximum size, required accuracy and production capacity before a configuration is recommended.
Before cutting anything, confirm:
Part CAD Revision = 2D Drawing Revision = Test Requirement
This sounds basic, but revision errors can invalidate an entire test.
A useful project record might contain:
Customer: ABC Automotive
Part Number: BP-RH-02
3D CAD Revision: F
2D Drawing Revision: F
Fixture Revision: B
NC Program Revision: P04
Test Date: 2026-xx-xx
If the drawing changes during the project, the old result should not automatically be treated as validation of the new revision.
Do not validate a machine using only a simple supplier demonstration sample.
A generic demo may prove that:
It does not prove that the machine can process your specific component.
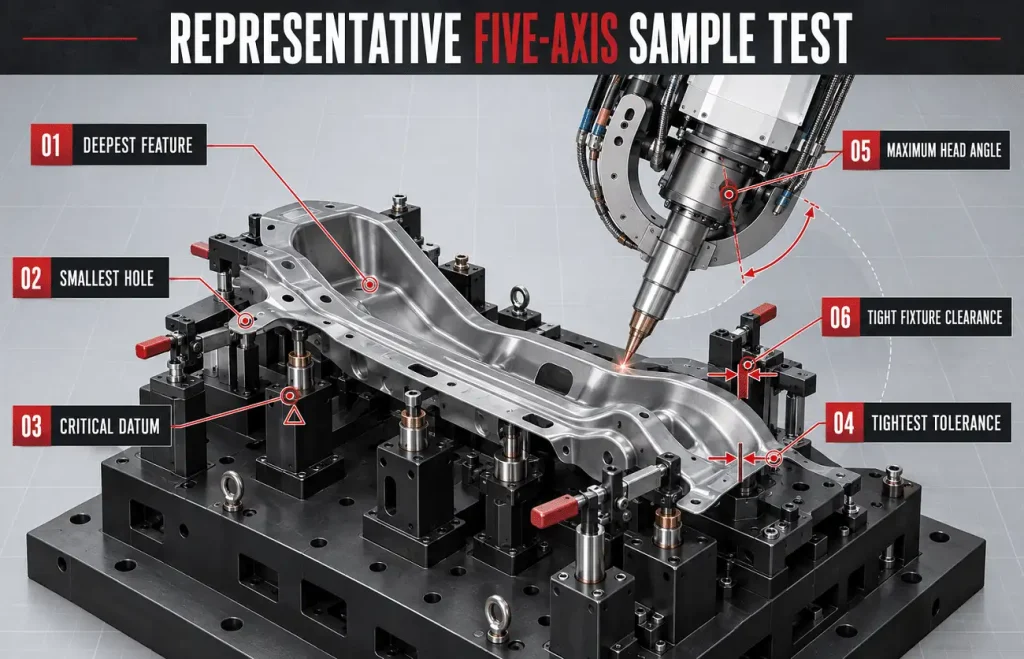
A representative validation part should contain the important production challenges.
These may include:
For hot-formed automotive projects, use production-representative formed components whenever possible.
Imagine a component contains:
The recessed hole should be one of the primary validation targets.
Similarly, identify:
A machine that performs 95% of the geometry but cannot process one functionally critical feature is not a successful solution.
This principle is already included in ZG Laser’s current five-axis buyer guide: difficult access areas should drive feasibility testing rather than only easy external contours.
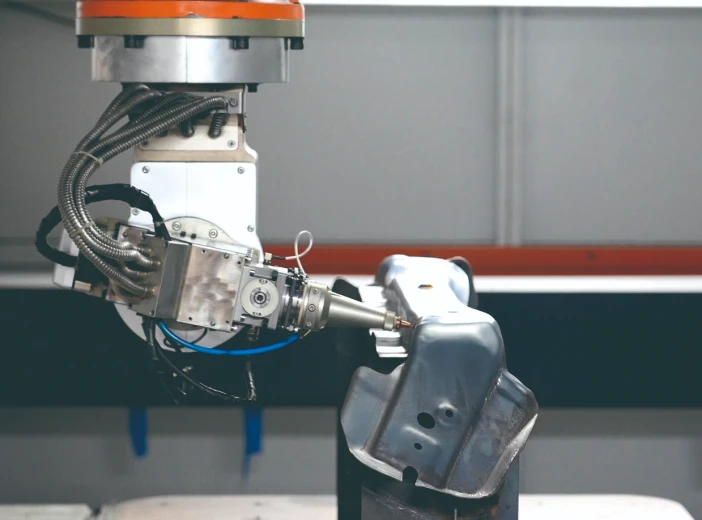
Image: Representative sample testing for a 3D five-axis laser cutting machine
Do not perform the test first and decide afterward what counts as acceptable.
Before sample cutting, both sides should agree on measurable criteria.
Examples include:
The important principle is:
Acceptance criteria should be agreed before the results are known.
This protects both buyer and supplier.
Not every dimension needs the same acceptance priority.
Identify:
Examples:
Examples:
This helps prevent a test from focusing heavily on an easy cosmetic edge while ignoring a critical hole position.
A useful FAT drawing can visually mark critical features.
A dimension has meaning only relative to its defined datum system.
Before testing, agree on:
The manufacturing fixture and inspection process do not necessarily need to be identical, but their datum relationship must be clearly understood.
Renishaw’s process-setting guidance similarly emphasizes establishing the relationship between machine, part and coordinate system through datum features before production begins.
This is particularly important for formed sheet-metal parts.
A component may be measured:
The result can differ.
A thin formed panel may meet dimensional requirements while constrained by the cutting fixture but move slightly after unclamping.
This does not automatically indicate a machine problem.
The drawing and customer quality standard should define the required inspection state.
Do not wait until FAT to discover that:
Supplier measured on fixture
while:
Customer expected free-state measurement.
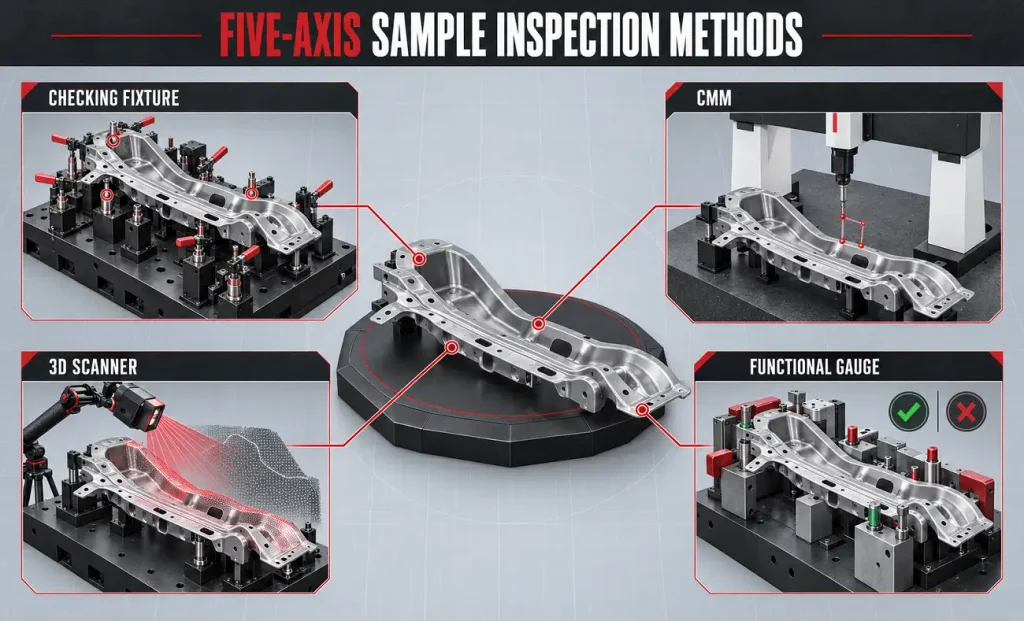
Possible measurement methods include:
Choose the method according to:
For tight dimensional criteria, the measuring method itself must be sufficiently capable and properly calibrated.
Do not claim machine failure from measurement data whose uncertainty is too large for the tolerance being evaluated.
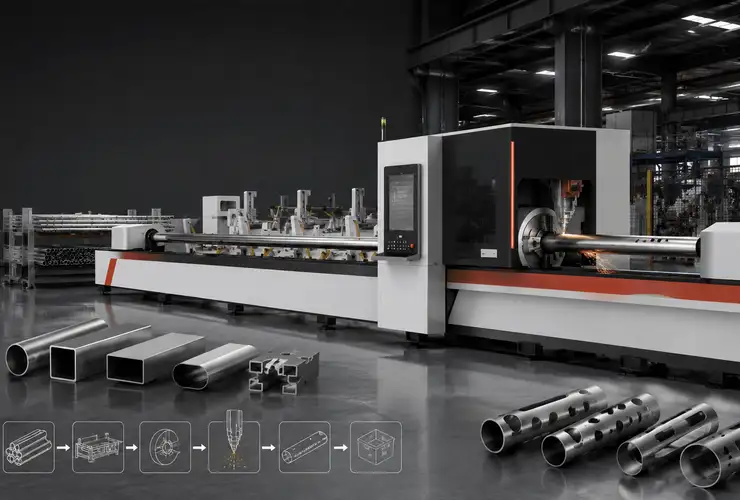
Image: Inspection methods for five-axis laser cutting sample validation
A poor fixture can make a good machine appear inaccurate.
Before evaluating cut dimensions, verify:
The fixture should locate the component consistently without forcing it into an artificial geometry.
Before cutting several production samples, it can be useful to test the fixture itself.
A simple method is:
This helps separate:
Fixture loading variation
from:
Part-to-part incoming variation.
If the same component does not return to the same position consistently, cutting more samples will not solve the underlying fixture problem.
The sample test should confirm that the complete laser head can reach every feature.
Check:
A successful offline simulation is very valuable, but the real fixture and machine should still be verified before full-speed production.
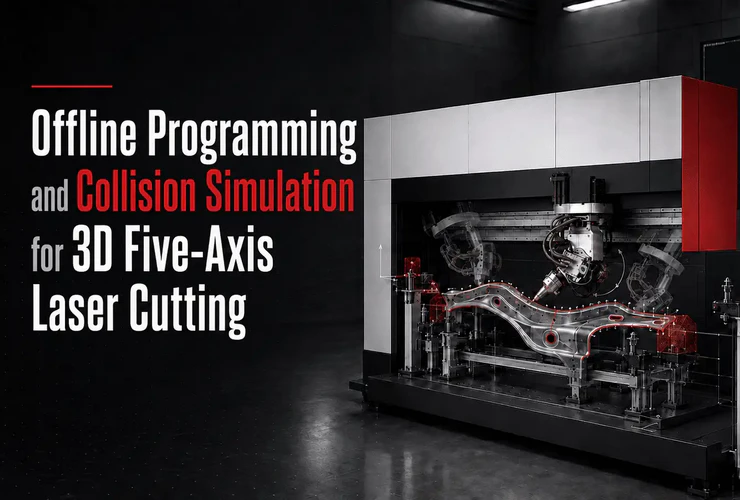
Offline programming and collision simulation
This is essential.
The validation record should identify:
Imagine a sample is tested successfully using:
6000W + production rotary table + one head configuration
but the commercial quotation later specifies:
3000W + different table + different cutting head
The original result should not automatically be considered proof of the quoted configuration.
A sample test validates a specific process configuration.
Important parameters can include:
This creates a process record.
Without these details, a successful sample may be difficult to reproduce later during FAT or SAT.
Fixtures often change during development.
For example:
Rev A
→ clamp interferes with cutting head.
Rev B
→ clamp moved.
Rev C
→ new support added to improve repeatability.
The test report should therefore identify the fixture revision used.
Otherwise, a later FAT may unknowingly use a modified fixture and be compared with results produced under different conditions.
The same principle applies to programming.
A production record should contain:
This is particularly important after:
A useful production rule is:
Approved part + approved fixture + approved program + approved parameters = validated process configuration.
Do not validate productivity using laser-on time alone.
Record:
Total Cycle Time = Loading + Positioning + Clamping + Table Movement + Piercing + Cutting + Repositioning + Unclamping + Unloading
For rotary-table production, also determine whether loading can occur in parallel with cutting.
| Stage | Time |
|---|---|
| Loading | — |
| Clamping | — |
| Table indexing | — |
| Cutting | — |
| Unclamping | — |
| Unloading | — |
| Total cycle | — |
Do not enter hypothetical values in the published article; use the real project data during validation.
A sample may look successful while requiring constant manual assistance.
Record whether the operator needed to:
A production process requiring repeated intervention may not achieve the same throughput as an ideal demonstration cycle.
A single successful sample answers an important question:
Can this machine and process manufacture the part under these conditions?
That is valuable.
But it does not prove:
Therefore, describe one part correctly:
Feasibility sample
rather than:
Mass-production capability proof.
The next step is to process multiple components using the same approved conditions.
Measure the same critical features on each part.
Record:
This allows you to see whether results are:
A small group of consecutive samples can provide useful repeatability evidence.
It should not automatically be presented as a formal statistical process-capability study.
If Cp, Cpk, Pp, Ppk or another capability metric is contractually required, define:
before the study begins.
Part-to-part variation can come from several sources.
Conceptually:
Production Variation = Machine + Calibration + Fixture + Incoming Part + Laser Process + Measurement
For example, if hole position varies between samples, possible causes include:
Do not immediately conclude that every variation is machine-axis error.
What determines 3D five-axis laser cutting accuracy
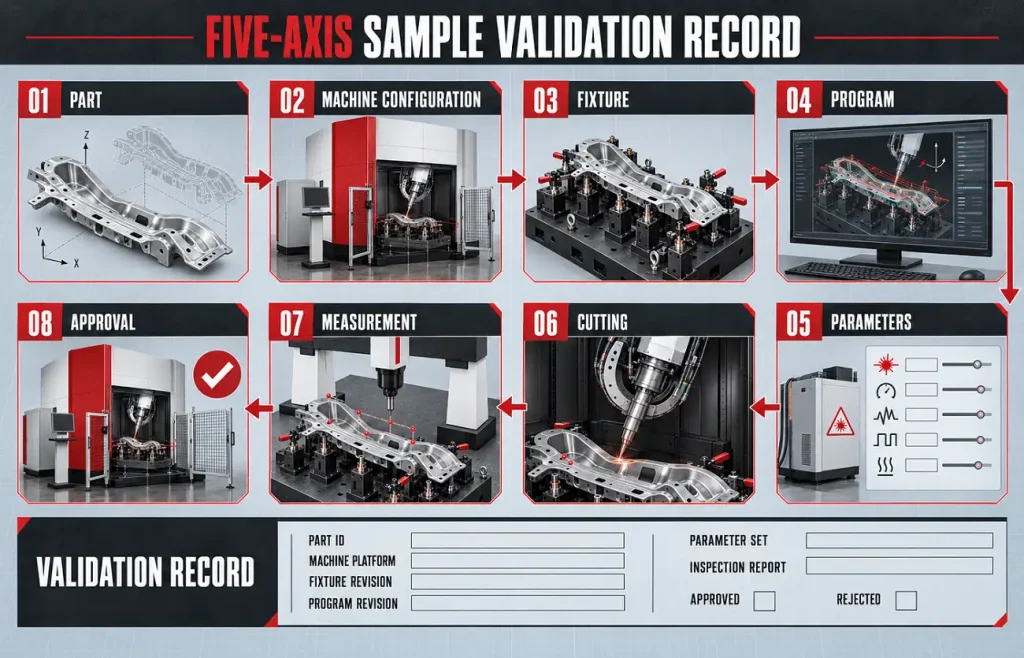
A structured report may include:
| Item | Record |
|---|---|
| Customer | Project name |
| Part | Part number |
| Drawing | Revision |
| CAD | Revision |
| Material | Grade |
| Thickness | Actual |
| Machine | Model |
| Laser | Source / power |
| Cutting head | Model/configuration |
| Fixture | Revision |
| NC program | Revision |
| Assist gas | Type |
| Test part | Sample ID |
| Cycle time | Complete cycle |
| Inspection method | CMM / gauge / etc. |
| Measurement result | Recorded values |
| Edge quality | Result |
| Operator intervention | Record |
| Deviations | Record |
This report becomes useful later during FAT.
Image: Five-axis laser cutting sample validation and test record
A Factory Acceptance Test, or FAT, is performed at the supplier’s facility before shipment.
For a custom five-axis laser project, FAT should normally verify two levels.
Does the delivered machine match the ordered configuration and operate correctly?
Can the completed system execute the agreed customer process?
This distinction matters.
A machine can pass a mechanical FAT while still failing the customer’s application requirement.
For application-specific equipment, both levels should be considered in the acceptance agreement.
Typical machine-level FAT items may include:
The exact list should match the signed technical agreement.
For a customized 3D cutting project, this is often the more valuable section.
Possible acceptance items include:
The customer and supplier should agree which items are binding acceptance criteria and which are engineering observations.
Do not copy an online FAT template and assume it is sufficient.
A B-pillar production line and a prototype aerospace cell may require very different acceptance tests.
The checklist should reflect:
If the project does not require a particular test, do not create unnecessary acceptance risk.
If a requirement is critical, make sure it is written into the agreement before machine completion.
A professional FAT record can contain:
Photographs or video may also be included where appropriate.
This is critical.
The system tested during FAT should correspond to the system being delivered.
If a temporary component is used during testing, document it.
Examples:
The buyer should know whether the FAT result represents:
final delivery configuration
or:
temporary engineering configuration.
A failed test does not automatically mean the entire machine concept is wrong.
Classify the problem first.
Examples:
Check:
Examples:
Check:
Check:
Check:
Check:
A structured root-cause investigation is more useful than random parameter adjustment.
Suppose the agreed hole-position requirement is X.
After testing, the result does not meet X.
The wrong response is:
“Maybe X was too strict; let’s call this acceptable.”
unless the customer engineering team formally changes the requirement.
Likewise, the buyer should not introduce a previously undisclosed tighter requirement only after seeing successful results.
The fair principle is:
Agree first. Test second. Judge against the agreed criteria.
These two samples serve different purposes.
Useful for showing:
It is primarily a capability demonstration.
Useful for evaluating:
For equipment purchasing, the second is much more valuable.
Remote FAT can be practical when:
A remote FAT package may include:
Show:
Avoid relying only on edited promotional video.
Customer attendance at the supplier’s factory deserves consideration for:
Being physically present can make it easier to review:
But attendance should be decided according to project risk rather than treated as mandatory for every machine.
After FAT approval, the machine is:
The final factory introduces different:
Therefore, final site verification is still important.
SAT verifies the installed system at the customer’s factory.
Typical SAT areas include:
| FAT | SAT |
|---|---|
| Supplier factory | Customer factory |
| Before shipment | After installation |
| Supplier utilities | Customer utilities |
| Confirms ordered machine | Confirms installed machine |
| Application test under supplier conditions | Application test under real site conditions |
| Pre-shipment acceptance | Final site acceptance |
The exact commercial meaning of FAT and SAT should be defined in the contract.
Do not assume that the terminology automatically creates the same obligations in every purchase agreement.
The relationship between:
must remain correct.
Transport and installation are therefore followed by machine setup and verification.
Renishaw’s process-control guidance emphasizes establishing machine, fixture, rotary-axis and workpiece relationships before machining, while its broader process-control framework separates process setting from post-process inspection.
For a five-axis laser system, follow the machine manufacturer’s installation and calibration procedure rather than simply copying the supplier-factory offsets.
A process validated during FAT can behave differently if the customer’s utilities are insufficient.
Check:
Where relevant:
These factors belong to the complete production system.
For the agreed validation part, compare:
The goal is not necessarily to reproduce every microscopic measurement identically.
The goal is to confirm that the installed process meets the agreed acceptance requirement.
If results differ materially, investigate:
before changing the acceptance criteria.
Offline simulation can significantly reduce machine-side prove-out.
Modern CNC digital-twin systems can model:
and detect potential collisions before production. Siemens’ current Run MyVirtual Machine and NX machine-simulation solutions specifically support complete machine models, NC validation, collision detection and realistic cycle-time calculation.
This is extremely valuable.
But simulation cannot fully reproduce every physical condition, including:
Therefore:
Virtual validation reduces physical risk; physical validation confirms the real process.
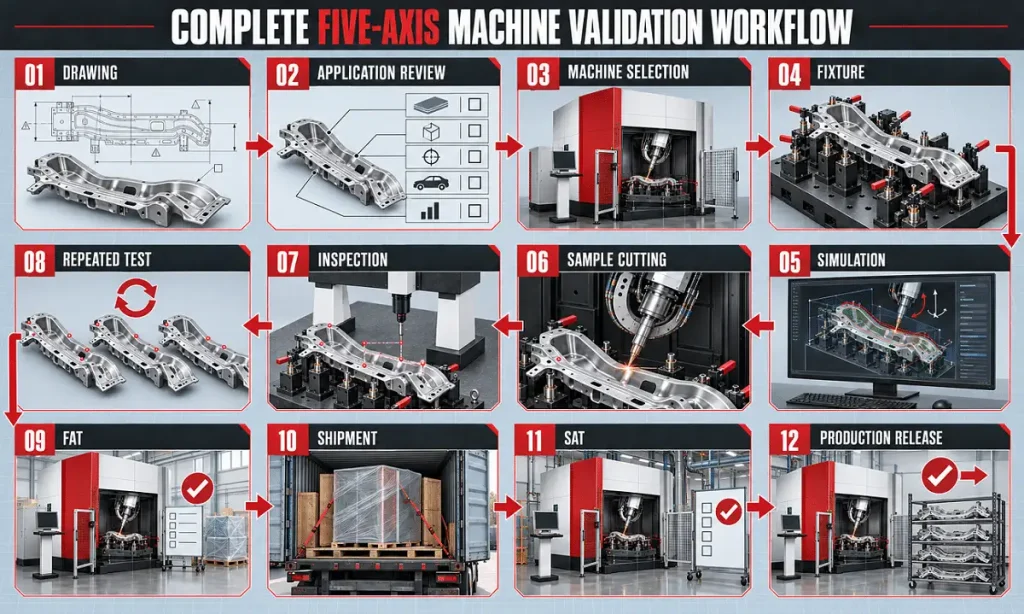
A strong project can follow this sequence:
Customer Drawing
↓
Application Review
↓
Machine Configuration
↓
Fixture Concept
↓
Offline Programming
↓
Collision Simulation
↓
Sample Cutting
↓
Dimensional Inspection
↓
Repeated Samples
↓
Configuration Approval
↓
Machine Manufacturing
↓
FAT
↓
Shipment
↓
Installation & Calibration
↓
SAT
↓
Production Training
↓
Production Release
This is much more reliable than:
Buy machine → ship machine → see whether the part works.
Image: Sample testing FAT and SAT workflow for a five-axis laser cutting machine
A practical technical agreement can organize acceptance into six areas.
This structure helps prevent important requirements from being buried inside a long machine specification sheet.
Avoid contractual statements such as:
“Good cutting quality.”
“High accuracy.”
“Fast production.”
These are difficult to verify.
Where commercially necessary, replace them with agreed measurable criteria such as:
Use photographs or approved reference samples if visual criteria are difficult to describe numerically.
A claimed 90-second cycle can mean very different things.
Does the clock start when:
Does it stop when:
For meaningful comparison, define:
Cycle Start
and:
Cycle End
before FAT.
For example:
From start of loading of one production part to the point at which the machine is ready to begin the next equivalent cycle.
The exact definition should reflect the customer’s production system.
If cycle acceptance is important, document:
Otherwise, two tests can claim the same machine cycle while using very different labor.
For an application-specific project, useful handover information may include:
Not every project requires every document, but the scope should be agreed before shipment.
Before approving a critical five-axis project, confirm:
A five-axis laser cutting machine should not be validated by a brochure specification or one attractive demonstration video.
The strongest purchasing decision is based on a structured sequence of:
representative sample testing → dimensional inspection → repeated verification → FAT → SAT
Each stage answers a different question.
A single sample answers:
Can the process make the part?
Repeated parts begin to answer:
Can the process produce similar results consistently?
FAT answers:
Does the completed machine match the agreed pre-shipment machine and application requirements?
SAT answers:
Does the installed system perform correctly under the customer’s real factory conditions?
The most important rule is to define acceptance criteria before the test begins.
That includes:
A successful five-axis purchase is therefore not only about selecting the right machine.
It is about creating an agreed and traceable path from:
customer drawing
to:
validated production process.
Send ZG Laser:
Our application team can evaluate:
before the final machine configuration is approved.
Request a Sample Cutting Evaluation
Explore 3D Five-Axis Laser Cutting Machines
For critical or custom 3D applications, sample testing is strongly recommended because it can verify cutting-head accessibility, fixture strategy, dimensional results, edge quality and production feasibility on the actual part.
It can demonstrate feasibility, but it does not by itself prove repeated production stability. Repeated parts should be evaluated when repeatability is important.
There is no universal number for every project. The quantity should be defined according to production risk, tolerance, volume and the purpose of the test. A formal process-capability study requires a separately defined statistical plan.
Typical items include critical hole positions, hole sizes, trim-line locations, slots, edge condition and complete cycle time. The exact criteria should come from the customer’s drawing and production requirements.
FAT means Factory Acceptance Test. It is normally performed at the supplier’s factory before shipment to verify the agreed machine configuration, operation and, where specified, the customer’s application requirements.
No. Sample testing often occurs during process and equipment evaluation. FAT normally verifies the completed ordered machine before shipment.
SAT means Site Acceptance Test. It is performed after installation at the customer’s factory to verify machine installation, utilities, calibration and agreed production requirements under real site conditions.
For an application-specific five-axis project, including the agreed customer part can make FAT much more meaningful because machine operation alone does not prove the production application.
If cycle time is an important purchasing requirement, it should be explicitly defined in the technical agreement, including what actions are included in the measured cycle.
Because the reported feature position depends on its datum system. Different inspection references can produce different interpretations of the same component.
Yes. Flexible or formed components may change shape after unclamping. The required inspection state should therefore be defined before acceptance testing.
No. Digital simulation can substantially reduce collision and programming risk, but physical validation is still needed to account for real fixtures, incoming-part variation, process behavior and other physical conditions.
First identify whether the problem relates to geometry, fixture, calibration, cutting parameters, collision/accessibility, cycle time or incoming-part variation. Correct the root cause and repeat the agreed test where necessary.

English

French

German

Hindi

Italian

Japanese

Korean

Portuguese

Russian

Spanish
Tell us about your manufacturing challenges.
Our engineers will design a laser solution tailored to your exact requirements.